Industrial Salt Production
Efficient Solid-Liquid Separation with Pusher and Basket Centrifuges
01 Introduction
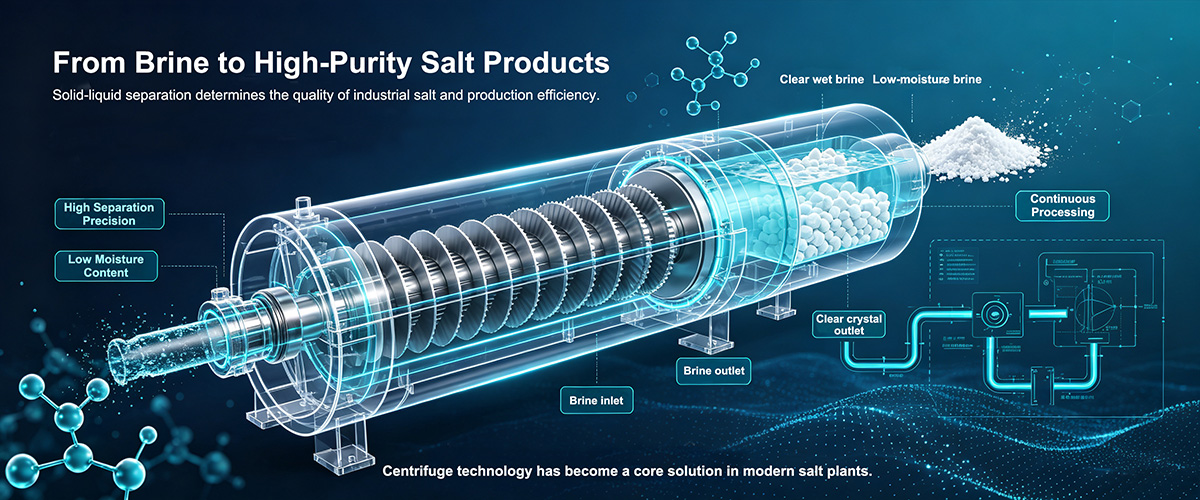
Industrial salt production requires high-efficiency separation systems to ensure product purity, low moisture content, and continuous production capability.
Centrifuge technology has become a core solution in modern salt plants.
02 Challenges in salt industry.
Salt processing plants often face:
* High crystal volume.
* Lower discharge limits.
* High moisture content.
* Continuous production requirements.
03 Why centrifuges are ideal for salt processing.
Continuous Operation
Especially suitable for large-scale salt production lines.
Stable Crystal Separation
Ensures uniform product quality.
Lower Moisture Content
Reduces drying energy cost.
High Durability
Suitable for corrosive environments.
04 Recommended equipment.
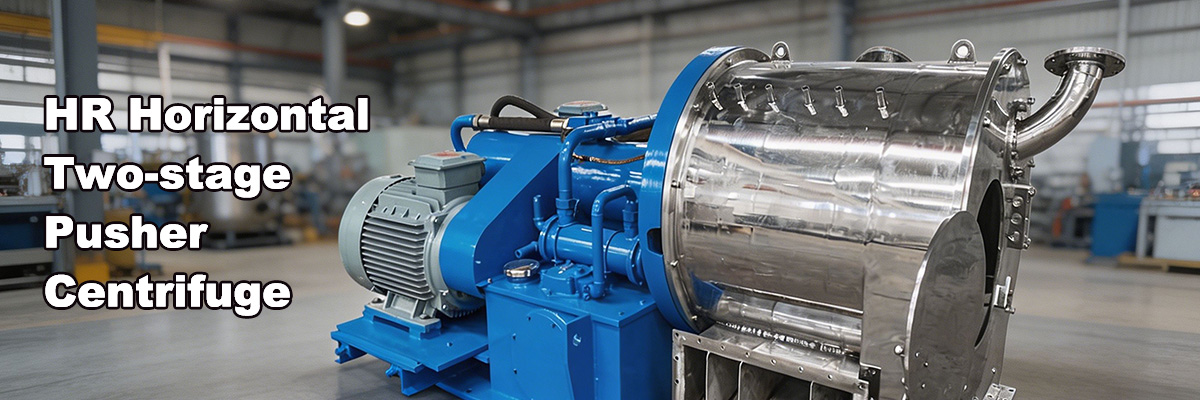
Pusher Centrifuge
Best for continuous high-capacity salt separation.
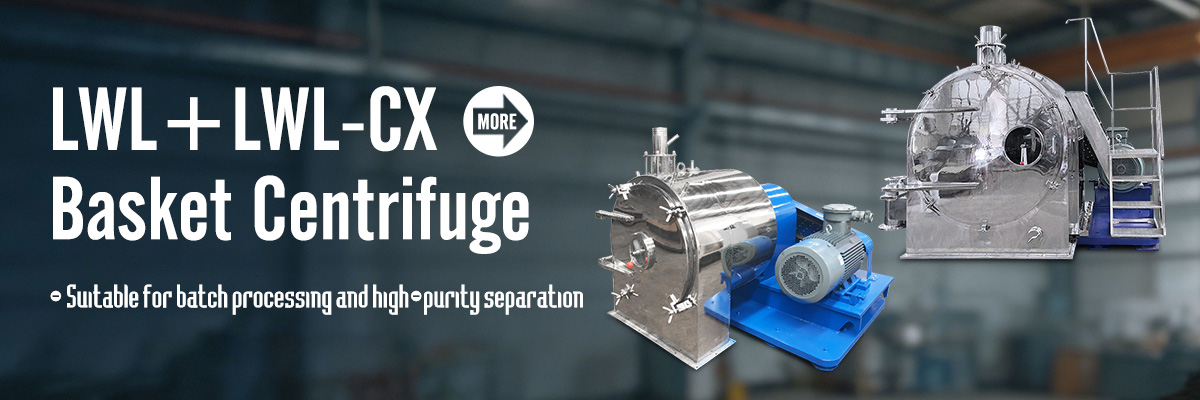
Basket Centrifuge
Suitable for batch processing and high-purity separation.
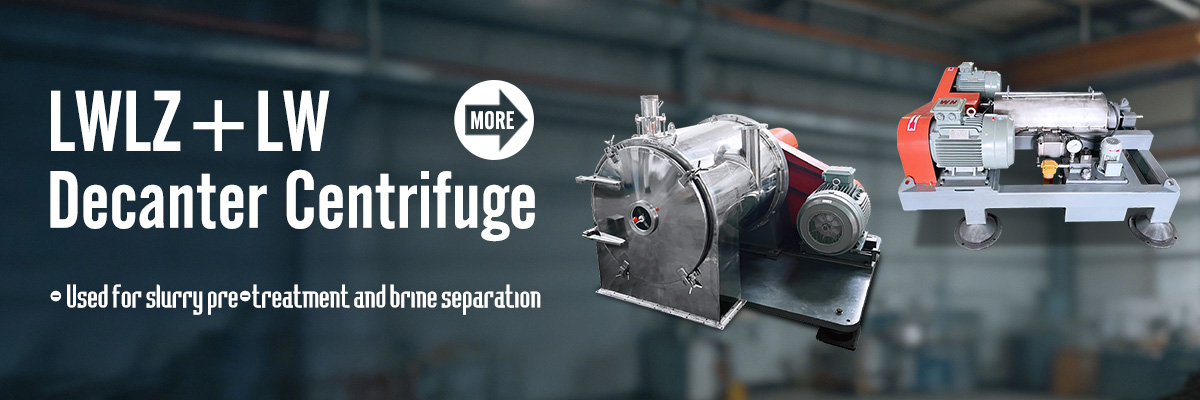
Decanter Centrifuge
Used for slurry pre-treatment and brine separation.
05 Industry applications.
* Sea salt production.
* Rock salt processing.
* Chemical salt purification.
* Industrial crystallization processes.
06 Conclusion.
With increasing global demand for industrial salt, centrifuge systems are becoming the preferred solution for efficient and continuous production.
07 Real Case Study:Zero-Discharge Wastewater Treatment Retrofit for a Chemical.
📞 Get in Touch: www.lnlxj.com
✅ Complimentary material analysis.
✅ Free on-site sludge testing.
✅ Tailored model selection & solutions.
✅ Quotation delivered within 24 hours.

30 Year Brand
A Number of National Patents

Contact Us
Know More