Centrifuge technology innovation under the trend of environmental protection
According to a report by the World Health Organization (WHO), the average annual wastewater treatment cost of chemical companies worldwide exceeds US$2 million, of which energy consumption accounts for as much as 30%-40%. With increasingly stringent environmental regulations, companies are facing huge cost pressures. How to reduce energy consumption and improve efficiency has become the core challenge of industrial wastewater treatment.
01 Traditional Separation Equipment and High-efficiency Centrifuges
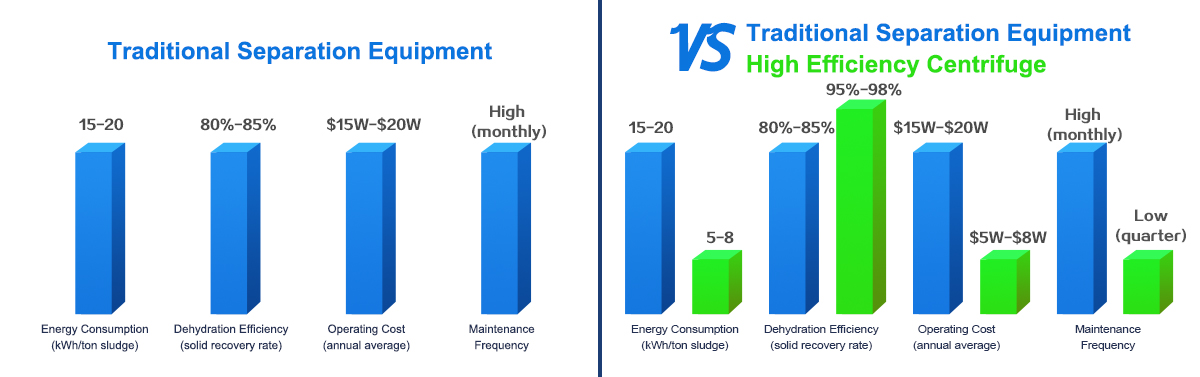
Traditional separation equipment (such as plate and frame filter presses and belt filter presses) has problems such as high energy consumption, low efficiency, and high maintenance costs in sludge dewatering. In contrast, high-efficiency centrifuges perform outstandingly in terms of energy consumption and efficiency:
|
Indicators |
Traditional separation equipment |
High efficiency centrifuge |
|
Energy consumption (kWh/ton sludge) |
15-20 |
5-8 |
|
Dehydration efficiency (solid recovery rate) |
80%-85% |
95%-98% |
|
Operating cost (annual average) |
$150,000-$200,000 |
$50,000-$80,000 |
|
Maintenance frequency |
High (monthly downtime for maintenance) |
Low (maintenance once a quarter) |
02 Case Story
Green transformation of European pharmaceutical companies
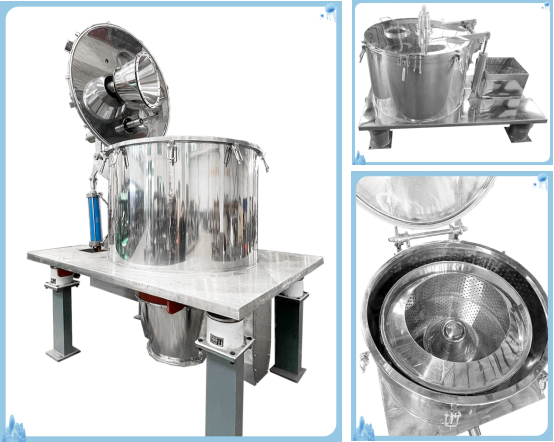
Recently, Blovebird has reached an in-depth cooperation with a well-known pharmaceutical customer. It has successfully achieved efficient treatment and reuse of pharmaceutical wastewater by using our independently developed high-efficiency separation equipment, the LWL series horizontal screen scroll centrifuge. With its innovative separation technology and excellent performance, this series of equipment helps customers achieve significant resource savings and cost optimization in the wastewater treatment process.
Through the application of the LWL series equipment, the company not only significantly reduced the comprehensive cost of wastewater treatment, but also achieved a 30% saving in energy consumption, further reduced carbon emissions, and promoted green production. At the same time, the efficient separation capacity of the equipment has enabled the water resource recovery rate to reach 60%, significantly improving the recycling rate of water resources, and creating considerable economic and environmental benefits for the company.
03 Customer Evaluation
“The high-efficiency centrifuge has helped us achieve the green transformation of wastewater treatment, which not only reduced costs, but also improved the company’s sustainable development image.”—— Head of the environmental protection department of a European pharmaceutical company
04 Tweet Interactive
“Is your factory facing the cost pressure of wastewater treatment? Leave a message in the comment area to challenge and get a customized solution for free!
05 Extended Discussion
Future trends in centrifuge technology
Intelligent: Through sensors and AI algorithms, real-time monitoring and optimization of operating parameters are achieved to further reduce energy consumption.
Modular design: Easy to install and maintain quickly, reducing downtime.
Green materials: Made of environmentally friendly materials to reduce the carbon footprint of the equipment during its life cycle.

30 Year Brand
A Number of National Patents

Contact Us
Know More